Liquid Cold Plate Machining for Laser Systems
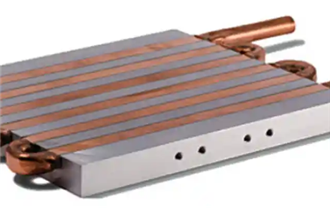
Date:2026-09-18Article editor:Starting Point PrecisionViews:17Laser systems generate intense heat during operation. Without efficient thermal management, performance drops, beam quality degrades, and components fail prematurely. Liquid cold plates solve this problem by transferring heat away from critical laser components through a circulating coolant. The machining quality of these cold plates directly determines how well the entire thermal system performs.
This article explains the key considerations for machining liquid cold plates used in laser systems, covering materials, design features, manufacturing processes, and quality control.
High-power lasers—whether diode, fiber, or solid-state—convert a significant portion of input energy into waste heat. Key heat sources include:
● Laser diodes and bars – sensitive to temperature changes
● Optical mounts and mirrors – thermal expansion misaligns optics
● Power electronics – drivers and controllers generate continuous heat
● Pump chambers – in solid-state systems
Air cooling reaches its limits beyond a few hundred watts. Liquid cold plates handle heat fluxes that air cannot, maintaining stable temperatures within ±0.5°C in many laser applications.
| Material | Thermal Conductivity | Machinability | Typical Use |
| Copper C110 | ~390 W/m·K | Good | High-power diode lasers |
| Aluminum 6061 | ~167 W/m·K | Excellent | Fiber laser housings |
| Aluminum 5083 | ~117 W/m·K | Good | Corrosion-resistant applications |
| Copper-tungsten | ~180-230 W/m·K | Difficult | CTE-matched optics mounts |
Copper offers superior heat transfer but weighs more and costs more to machine. Aluminum provides a better strength-to-weight ratio and is easier to machine, making it common for fiber laser cooling assemblies. Material selection depends on heat flux, weight constraints, and compatibility with the coolant.
Liquid cold plates for lasers require several precision features:
● Microchannel or minichannel geometries – increasing surface area for heat transfer
● O-ring grooves – sealing against leaks under pressure
● Flatness tolerances – often 0.02 mm or tighter for direct component mounting
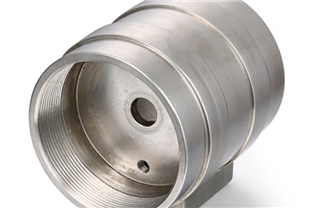
● Threaded ports – for fittings and coolant connections
● Mounting holes – positioned to align with laser modules
These features demand tight tolerances. A warped cold plate creates air gaps that reduce thermal contact. A poorly sealed channel leaks coolant onto sensitive optics.
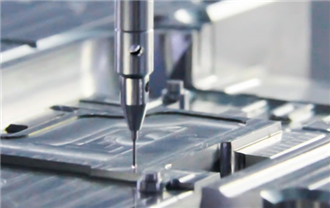
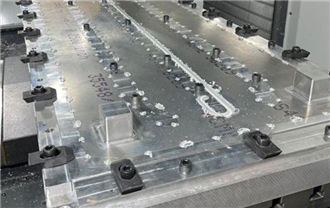
1. CNC machining – mills channels, ports, and mounting features
2. Friction stir welding – joins cover plates to channeled bases
3. Vacuum brazing – alternative joining method for complex internal geometries
4. Surface finishing – fly cutting or lapping to achieve flatness
5. Leak testing – pressure decay or helium mass spectrometry
6. Cleaning – removing chips, oils, and particles before assembly
Each step affects thermal performance. For example, cold plate design principles emphasize minimizing thermal resistance at every interface.
A reliable cold plate must pass:
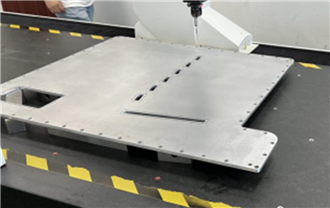
● Dimensional inspection (CMM)
● Flatness measurement
● Pressure testing (typically 1.5× working pressure)
● Helium leak detection
● Flow rate and pressure drop verification
● Thermal cycling
For laser systems, helium leak testing is often mandatory. Even tiny leaks can contaminate optical surfaces or cause coolant loss during operation.
● Keep channel walls thick enough to withstand pressure but thin enough for heat transfer
● Avoid sharp internal corners that create stress concentrations
● Use turbulent flow promoters (e.g., fins or dimples) where heat flux is highest
● Match the cold plate's coefficient of thermal expansion (CTE) to the mounted component when possible
● Consider copper's thermal properties when calculating performance
| Laser Type | Cooling Challenge | Cold Plate Solution |
| Diode laser bars | High heat flux (>100 W/cm²) | Copper microchannel |
| Fiber laser | Distributed heat along fiber | Aluminum cold plate with multiple zones |
| Solid-state laser | Thermal lensing in crystal | Copper-tungsten mount with liquid cooling |
| Ultrafast laser | Peak power and thermal cycling | Low-CTE cold plate with tight flatness |
In-house machining of liquid cold plates is possible for simple designs. But laser systems often require:
● Tight flatness (≤0.02 mm)
● Leak-free joints
● Consistent channel dimensions
● Documented quality records
A specialized manufacturer can reduce risk and lead time. Start Precision provides CNC machining for thermal management components, including liquid cold plates for laser and photonics applications. Their capabilities cover prototyping through production, with inspection reports and material certifications.
Liquid cold plate machining for laser systems is a precision discipline. Material choice, channel design, joining method, and quality control all influence thermal performance and reliability. Whether you are developing a new laser product or improving an existing thermal solution, investing in properly machined cold plates protects your optics, extends component life, and maintains beam quality.
Contact us to discuss your manufacturing needs.
Q1: What is the best material for a laser cold plate?
Copper offers the highest thermal conductivity and is preferred for high-heat-flux diode lasers. Aluminum 6061 is a good choice for lower heat fluxes where weight matters.
Q2: How flat should a laser cold plate be?
For direct component mounting, aim for 0.02 mm or better across the mounting surface. Inadequate flatness increases thermal contact resistance.
Q3: What leak testing method is recommended?
Helium mass spectrometry is the most sensitive method and is often required for laser systems. Pressure decay testing is acceptable for less critical applications.
Q4: Can cold plates be machined from a single block?
Yes, single-block machining eliminates joint leaks but limits internal channel complexity. Welded or brazed assemblies allow more intricate channel designs.
Q5: What coolant is suitable for laser cold plates?
Deionized water with corrosion inhibitors is common. Some applications use glycol mixtures for freeze protection. Coolant choice affects material compatibility and thermal performance.
Add: Building 3No.277 Zhen'an Middle Road, Chang'an Town,Dongguan,Guangdong, China
Tel:+86-769-82855591
Copyright © 2019 All Rights Reserved Dongguan Start Precision Technology Co., Ltd. Tel: +86-769-82855591
Add: No. 277 Zhen'an Middle Road, Chang'an Town, Dongguan, Guangdong, China
 中文版
 English